Ryan • Published 06 2026 Aug
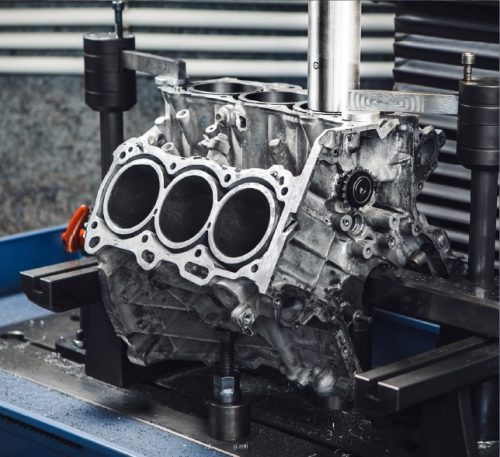
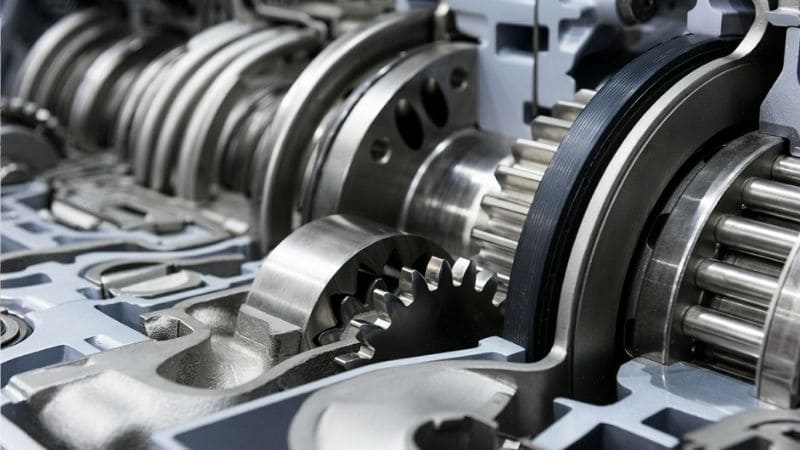
The same inspection approach applies to valve body machining and engine block machining.
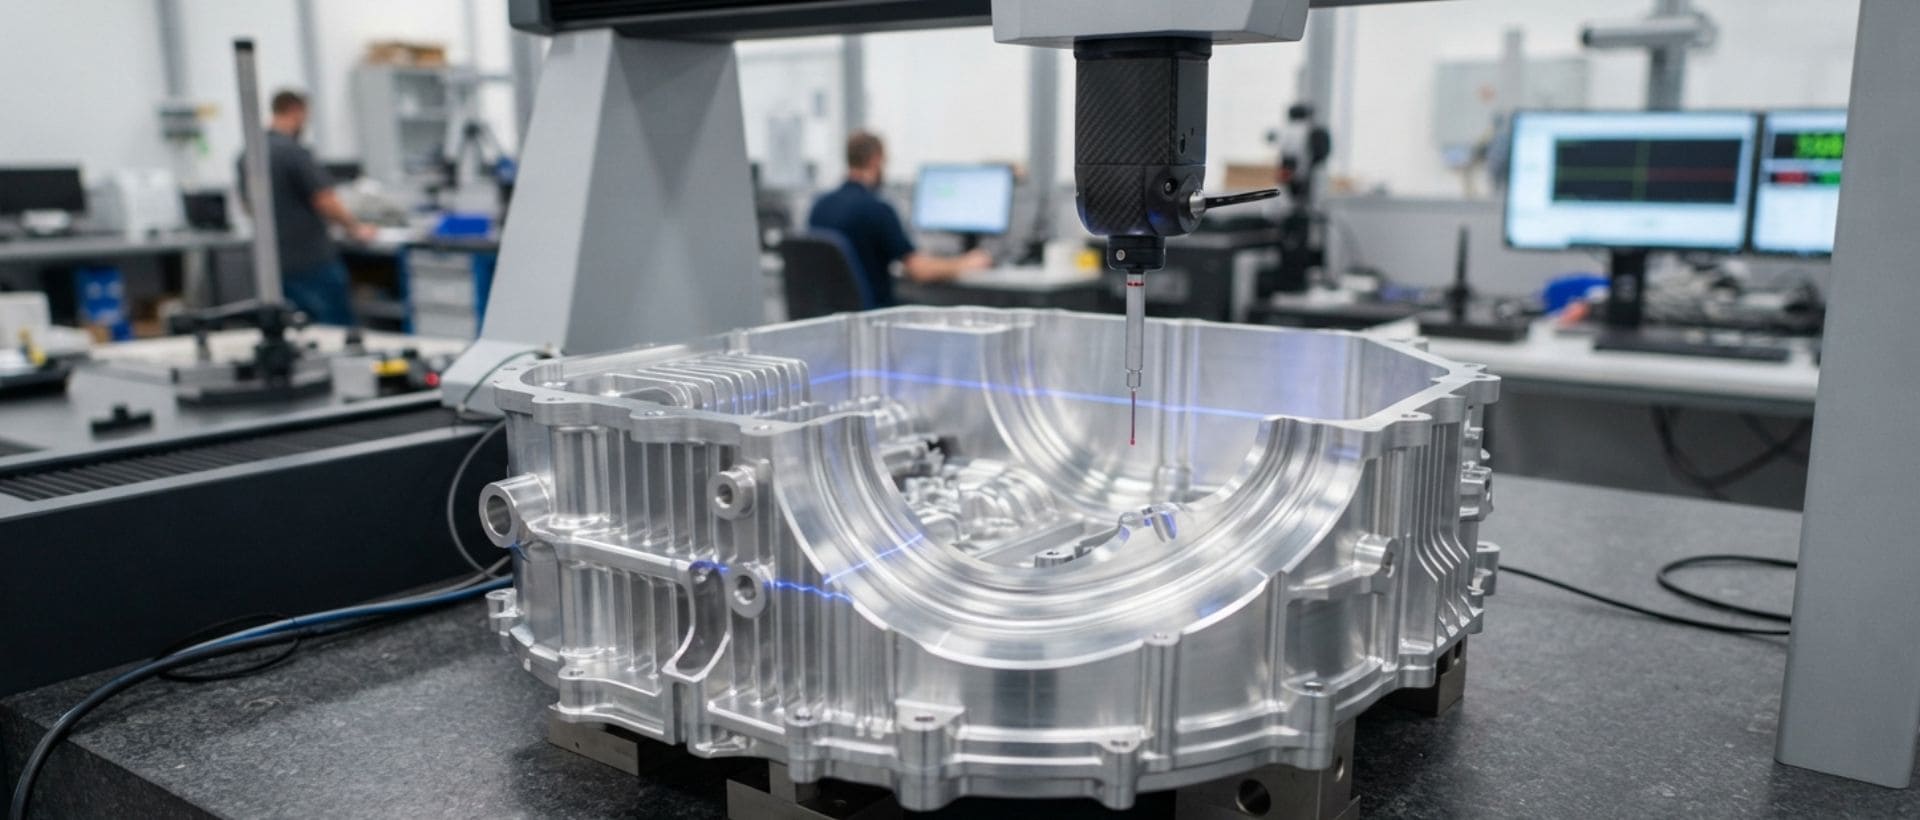
Complex automotive housings production demands stringent geometry control for long-term battery reliability. Advanced CMM inspection is primarily used to check these quotation mark profile and position tolerances. Strict dimensional tracking ensures that every detail component fits with mating assemblies.
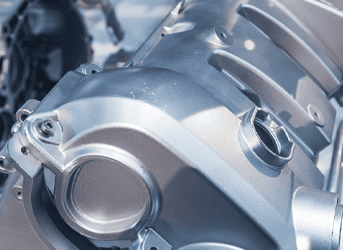
Complex automotive housings are engine compartments and battery casings made to hold mechanical, electrical, and electronic components. Because they protect sensitive mechanical and electronic systems, these components have complex geometries, thin walls, and tight location interfaces.
In production, effective geometric management of these characteristics is necessary so that there are no leaks of operational fluids, structural stresses are reduced, and smooth integration at final assembly is ensured.
Today’s automotive designs are based on stringent Geometric Dimensioning and Tolerancing (GD&T). That’s to make sure complex components function together under high working stresses. The automated coordinate metrology is the needed high-precision evaluation that is used to verify the numerous profile and position requirements via multiple datum reference frames.
Even small variations in dimensions on mating surfaces can disrupt sealing and cause critical leaks of fluids or electricity over time. By detecting these spatial offsets correctly early on, we prevent assembly interference downstream and protect the long-term mechanical reliability.
It’s impossible to access deep internal cavities or fully describe free-form organic curves using handheld tactile gauges and manual instruments. Advanced multi-axis probing systems overcome these physical limitations by capturing thousands of data points across complex internal configurations without distorting the part.
Identifying machining errors or thermal distortion during production prevents defective parts from entering the supply chain. The strict quality gate greatly reduces internal scrap rates and prevents the disastrous financial and reputational cost of field recalls.
Manufacturers need PPAP documentation to ensure that production of automotive parts is consistent. Digital inspection workflows automatically log/record complete/entire dimensional data, which regulatory authorities can trace right back to its source. And provides a concrete/theoretical statistical base/proof for quality audits.
Profile tolerance is a 3D error-limiting zone around a surface that controls size, shape, and orientation at the same time. This geometric checks that complex, freeform surfaces do not stray away from their nominal CAD design, thereby ensuring the separate parts mate flush without gaps. Restricting the whole surface area and not just certain linear points, complex section profiles remain functional while operating vehicles heavily.
Our measurement approach merges tactile probing with non-contact optical sensors for an immersive imaging of all housing geometries. When it comes to measuring critical datum features, tactile scanning can provide high accuracy reference data. Optical sensors are capable of quickly capturing thousands of data points across free-form surfaces that are very complex.
The densely packed point cloud is overlaid on the nominal CAD model to evaluate the dimensional variations. Advanced evaluation software converts these spatial coordinates into a colored map of deviations. This enables quality engineers to accurately identify where the component surface deviates from its design.
An area is characterized by its position tolerance for a feature of a size. Position tolerance is the zone within which the axis, center plane, or true position of a fastener hole, dowel pin locating bore, mating shaft aligning guide, etc., is permitted to vary from the theoretically exact location. For complex automotive housings, this control assures that points on multiple bolt patterns and important rotational centers in split-line assemblies coincide.
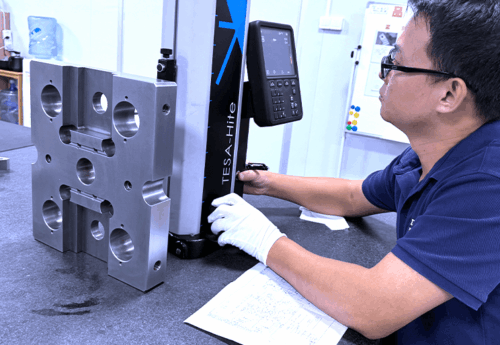
Position tolerance evaluation commences with a coordinate system based on the component’s primary, secondary, and tertiary datums. The machine then probes, locating bores and alignment slots to determine their exact center coordinates.
Metrology software will process these points to get the true position deviation from the datum reference. The bonus tolerance afforded by feature size deviation will be utilized by the system when a maximum material condition modifier is called out on the blueprint.
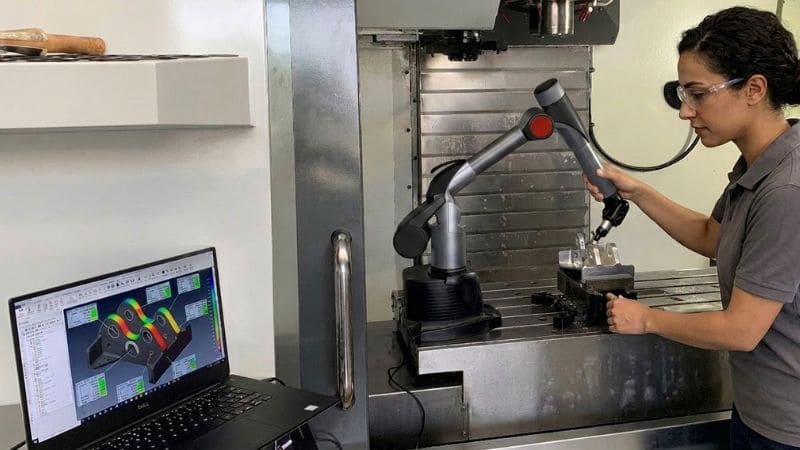
The inspection process entails importing the engineering CAD file and constructing a machine coordinate system with the reference point system or a certain datum feature to correspond with the physical component layout.
We choose the best sensor configuration, using high-accuracy contact probes for tight datum features and fast scanning heads for quick data across large surfaces.
The measuring system locates and targets individual geometric elements to measure important locator bores, flat mating planes, and alignment slots in the housing.
High-density scanning sensors capture millions of spatial data points throughout the entire component to document free-form contours and complex wall thicknesses.
Metrology software checks the coordinates collected with respect to the nominal CAD design to ensure that all the specified profile and position tolerances are followed strictly.
The system will generate data outputs, such as the first article inspection and production part approval process, to ensure the component meets all OEM requirements.
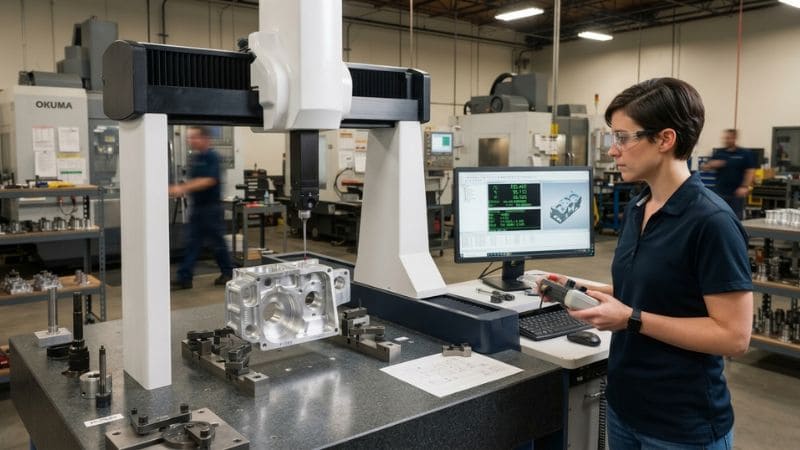
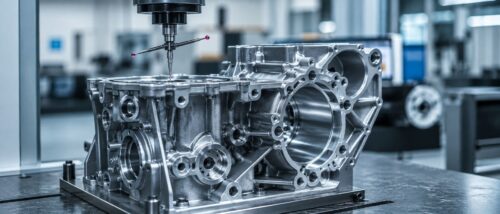
The systems use a solid moving component installed on granite that offers great mechanical stability and vibration decoupling. This rigid setup provides micron accuracy for the verification of components, including transmission housings and valve body features with tight tolerances.
Overhead rails elevate large and heavy workpieces and directly load them onto the floor substrate. This large measuring envelope effectively certifies the structural integrity of multi-piece enclosures for EV batteries and truck powertrain units.
The automated indexing head is designed to integrate a combination of tactile contact probes, optical sensors, and laser line scanners. Switching the sensor dynamically during the program run, rigid alignment features, and complex surface profiles can be evaluated without the need for re-fixuring of the part.
By shining a beam of light across the component, millions of points of surface data are captured every second without contact. This non-contact method allows for the speedy assessment of thin-walled areas and complex organic shapes that are easily distorted by touch probes.
A specialized analog probe glides effortlessly across the part surface while maintaining contact to gather a continuous data stream. Highly dense data enables the software to calculate form characteristics such as cylindricity and roundness, rather than isolated point calculation.
The components of aluminum or magnesium cast undergo dynamic expansion or contraction during measurement, due to ambient temperature variation in shop-floor environments. If these environmental variables are not controlled tightly or real-time compensation algorithms are not applied, then false rejects and unstable gauge repeatability will occur.
The complex oil channels and geometries inside the probe require extreme stylus lengths, which increase probe deflection and hinder measurement. Standard indexing heads mostly fail to reach deep yet safely enough into these cavities without crashing and damaging the hardware on the walls.
In practical applications, a tactile measurement force can mechanically deform sensitive thin-walled regions on light-weight structural components at the point of measurement. The physical introduction of distortion causes a misalignment of the coordinates in space and the profile of the part.
The process of validating the quality of materials and products based on a high density of data points often takes a long time. This is increasingly misaligned with the speeds at which automated production lines operate. Teams working in metrology must compromise between the desire for comprehensive and geometric verification versus the commercial reality of manufacturing throughput bottlenecks.
The part gets distorted, or the physical position of the part changes relative to the machine origin due to variable clamping force or minuscule debris on the location pins. The difference in the structural orientation introduces a measurement error that does not exist in the free error component.
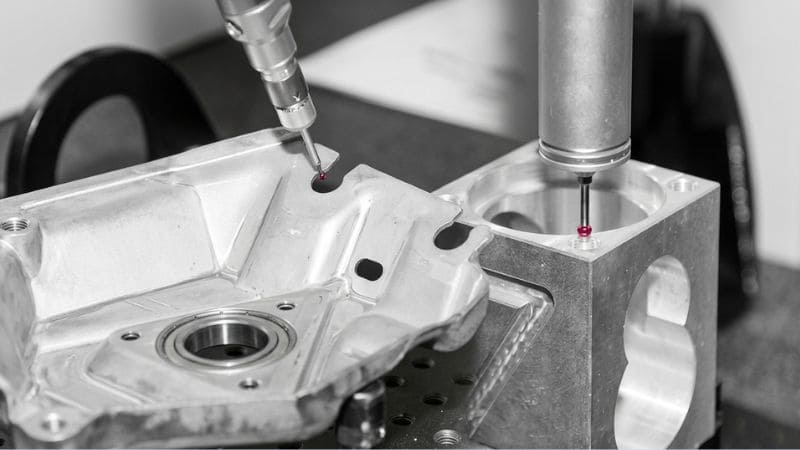
Real-time inspection data provides dimensional offsets directly to the production equipment. It automatically compensates for tool wear and thermal drift before parts are off-spec.
Finding small tolerance deviations early on in the production cycle prevents machining operations from taking place on already defective castings, saving on raw material as well as process cost.
By ensuring full geometric compliance histories for each serial number, digital inspection records provide the bulletproof validation documentation required during automotive safety audits.
Standardized metrology routines verify any raw or sub-assemblies coming in against the engineering design to ensure that external supply chains meet tier-one specifications.
Automated scanning workflows quickly execute complex confirmation processes, significantly reducing the time it takes to complete first article reports and gain production part approval.
Reference Point System alignments utilize well-defined coordinate points on free-form surfaces for precisely orienting the part as it attaches to the vehicle chassis, ensuring uniform repeatability.
Datum-based alignment fixes the coordinate system to precise geometric hierarchies, while best-fit alignment uses a mathematical process that averages deviations across the whole surface to assess unconstrained profiles.
You can import your own mathematical models, allowing the software to automatically calculate the vector paths and nominal point coordinates. This avoids any programming errors during initial set up.
Imposing automated routines for cleaning, loading, and execution minimizes human deviations and guarantees identical measurements during different shifts.
The machine’s reference origin is established immediately without the need to touch the part on dedicated holding nests with calibration spheres.
Our high-mix low-volume and high-volume mass production process is governed by strict adherence to IATF 16949 and ISO 9001 quality systems. Our early DFM support optimizes housing geometries for OEM-grade tolerance control at lower manufacturing costs. Each precision-machined component undergoes careful geometric dimensioning and tolerancing evaluation to provide complete inspection reporting and full automotive compliance certification.
Precision manufacturing involves complete metrological control, from strong datum definition to advanced surface scanning. Solving high-volume cycle times and thermal expansion problems is crucial to keeping the assembly line running without quality failures.
Get precision automotive machining and CMM inspection of your complex housings with DEK Automotive. Contact our experts to request a quote today.
Ryan oversees quality audits and advanced metrology for high-precision automotive machined parts. As an expert in First Article Inspection, CMM verification, and IATF 16949 standards, he ensures every milled and turned component is 100% reliable and ready for rigorous vehicle assembly testing.
We integrate advanced machining, specialized materials, and surface finishing to deliver mission-critical parts that meet every rigorous automotive standard.
Fill out the form below and our team will get back to you promptly with a personalized quote tailored to your needs.