Custom Connector Housing Machining

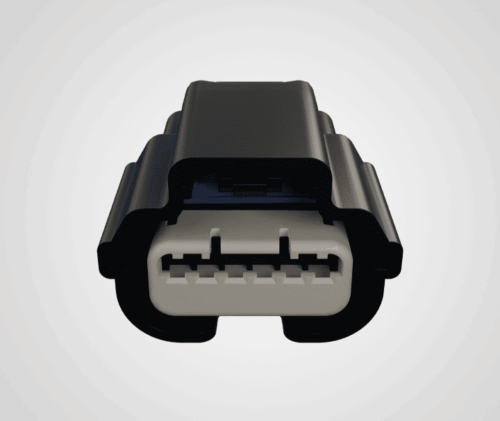
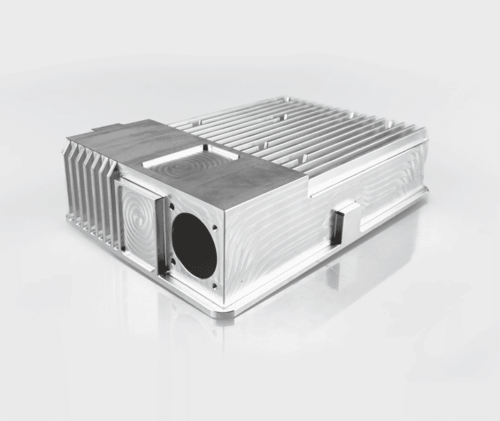
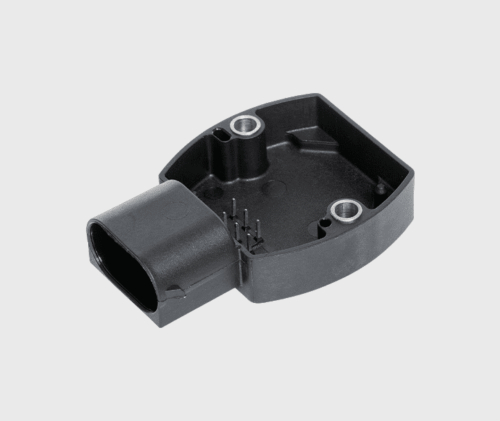
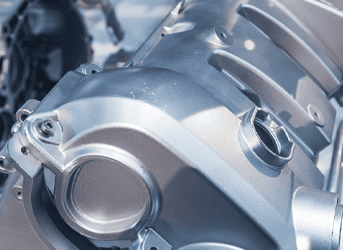
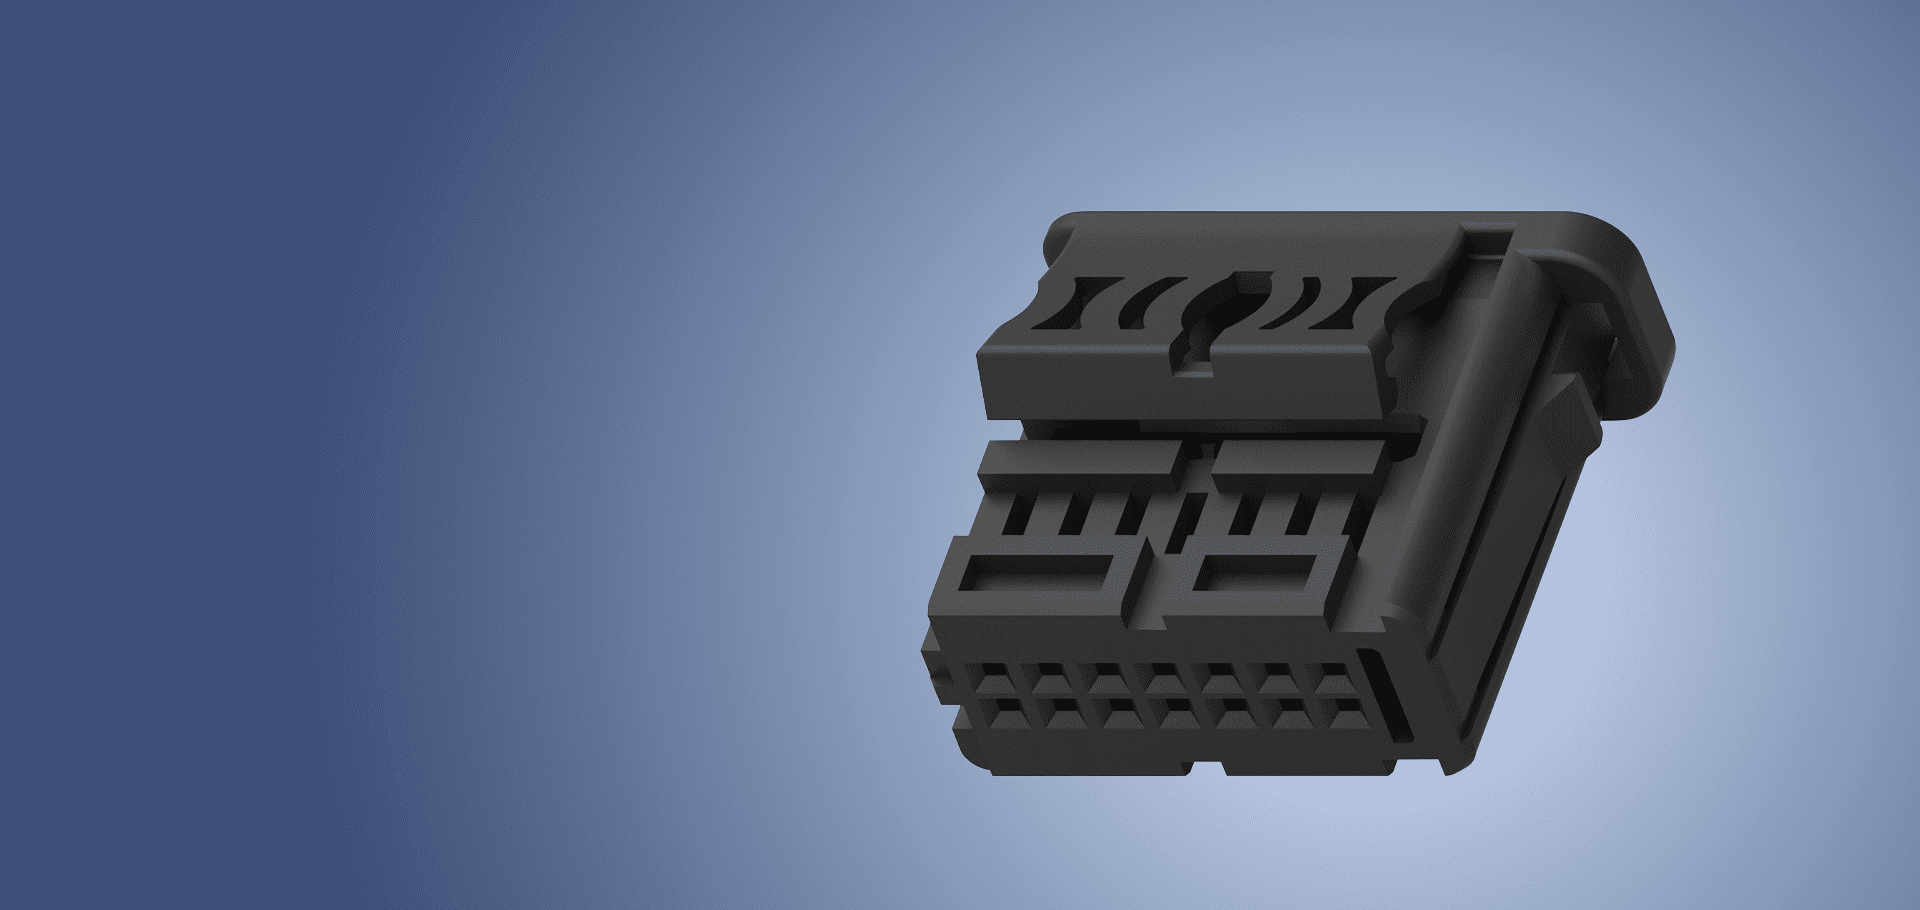
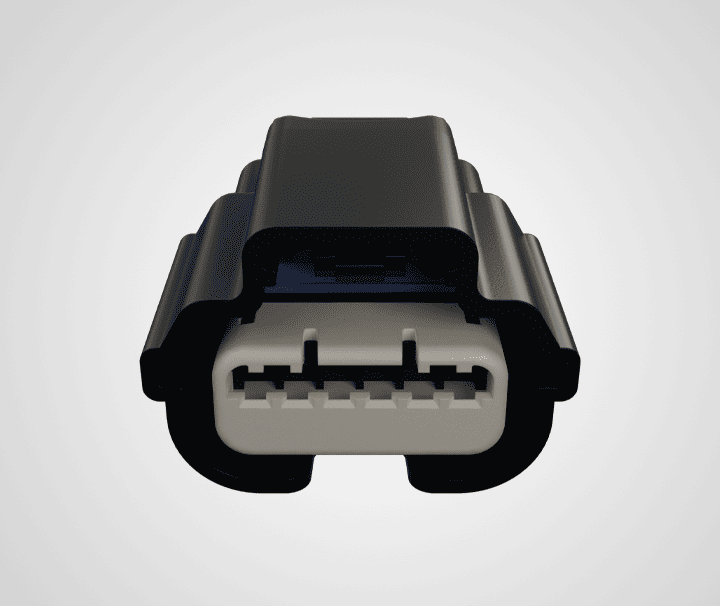
High-precision electrical connector housings built with high-grade alloy and tight tolerances for effective shielding in critical automotive wiring.
Contact Us
Overview

Reliable Automotive Electrical Connector Housing Production

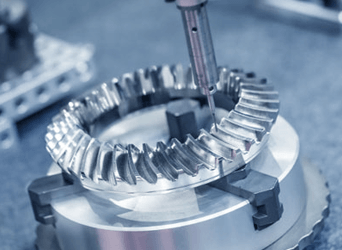
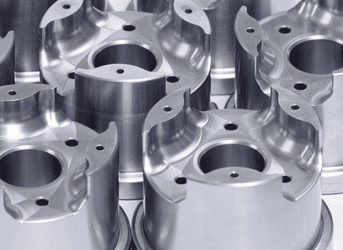
We manufacture precision-engineered connector housings utilizing advanced 5-axis CNC processes to achieve accurate terminal fitment and a reliable circuit. Every component undergoes rigorous inspection to meet IATF 16949 and ISO 9001 quality standards.

From rapid single-piece validation prototypes to scaled high-volume supply deployments, our production lines maintain strict batch consistency. We integrate comprehensive Design for Manufacturability (DFM) support alongside full PPAP documentation.

Contact Us
Challenge

Challenges & Solutions For Connector Housings

  • 01

    Pin Cavity Alignment

    We utilize specialized multi-point fixturing to machine terminal paths within a strict +/- 0.02 mm tolerance, preventing pin deformation during automated mating.

  • 02

    Contact Terminal Retention

    Locking channel geometries and internal retention ledges are milled to exact depths, providing a secure mechanical hold that resists vibration-induced terminal back-out.

  • 03

    Moisture Ingress Protection

    By finishing sealing lips and cable entry bores to controlled Ra 0.8 - 1.6 um specs, we ensure uniform seal compression for IP67 or IP69K ratings.

  • 04

    Thermal Cycling Distortion

    We machine uniform wall profiles from high-stability materials to prevent structural warping across extreme automotive operational temperatures ranging from -40°C to +150°C.

  • 05

    Complex Multi-Row Architecture

    Leveraging simultaneous 5-axis toolpaths allows us to mill deep, high-density cavity patterns and thin partition walls without risking tool deflection.

Capabilities

Connector Housing Technical Specs

Detailed dimensional and machining parameters we prioritize when qualifying high-precision connector housings for automotive electrical project.

Contact Us
Manufacturing Parameters Technical Specifications
Max Machining Dimensions (3-Axis) 500 × 400 × 300 mm
Max Machining Dimensions (5-Axis) 400 × 350 × 250 mm
Positional Cavity Tolerance ±0.02 mm True Position
Sealing Surface Roughness (Ra) Up to Ra 0.8 – 1.6 µm
Primary Process Materials Aluminum (6061-T6, ADC12), PA66-GF30, PBT
Minimum Partition Wall 0.9 mm between adjacent cavities
Thread and Insert Accuracy Metric sizes M2 to M10, ±0.02 mm
Related

Explore More Parts


Why Choose Us

Why Engineers Choose Our Connector Housings

  • 01

    Pin Cavity Integrity

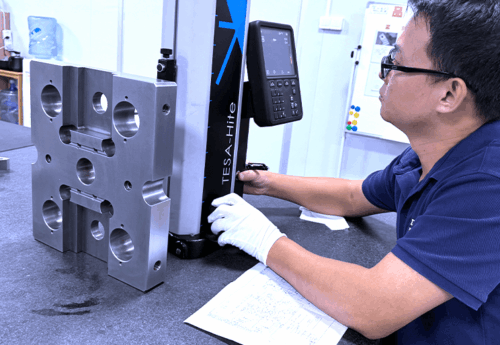
    Every cavity position verified by CMM to ±0.02 mm positional accuracy.

  • 02

    IP Rating Confidence

    Sealing profiles machined to geometry that sustains IP67 and IP69K ratings.

  • 03

    Temperature Range Stability

    Wall thickness and materials engineered to perform from -40°C to +150°C.
FAQs

Frequently Asked Questions

Contact Us
What primary materials are utilized for automotive electrical connector housings?
We machine structural 6061-T6 aluminum, die-cast ADC12, and glass-filled polymers selected for dimensional stability and high chemical resistance.
Can your facility maintain strict tolerances across complex multi-cavity bodies?
Yes, our 5-axis CNC centers achieve a precise +/- 0.05 mm positional accuracy, fully verified via automated CMM validation tracking.
Do you supply complete PPAP documentation for Tier 1 wiring programs?
We deliver full PPAP Level 3 compliance data, including material certifications, dimensional layouts, and end-to-end trace documentation.
How do you inspect the quality of critical sealing surface profiles?
Every sealing interface is verified using advanced contact profilometers to ensure matching roughness values conform to environmental sealing specs.
Are you able to process custom prototype designs directly from CAD models?
Yes, we accept standard STEP or IGES files, conducting a pre-production DFM check to optimize tolerances before cutting metal.