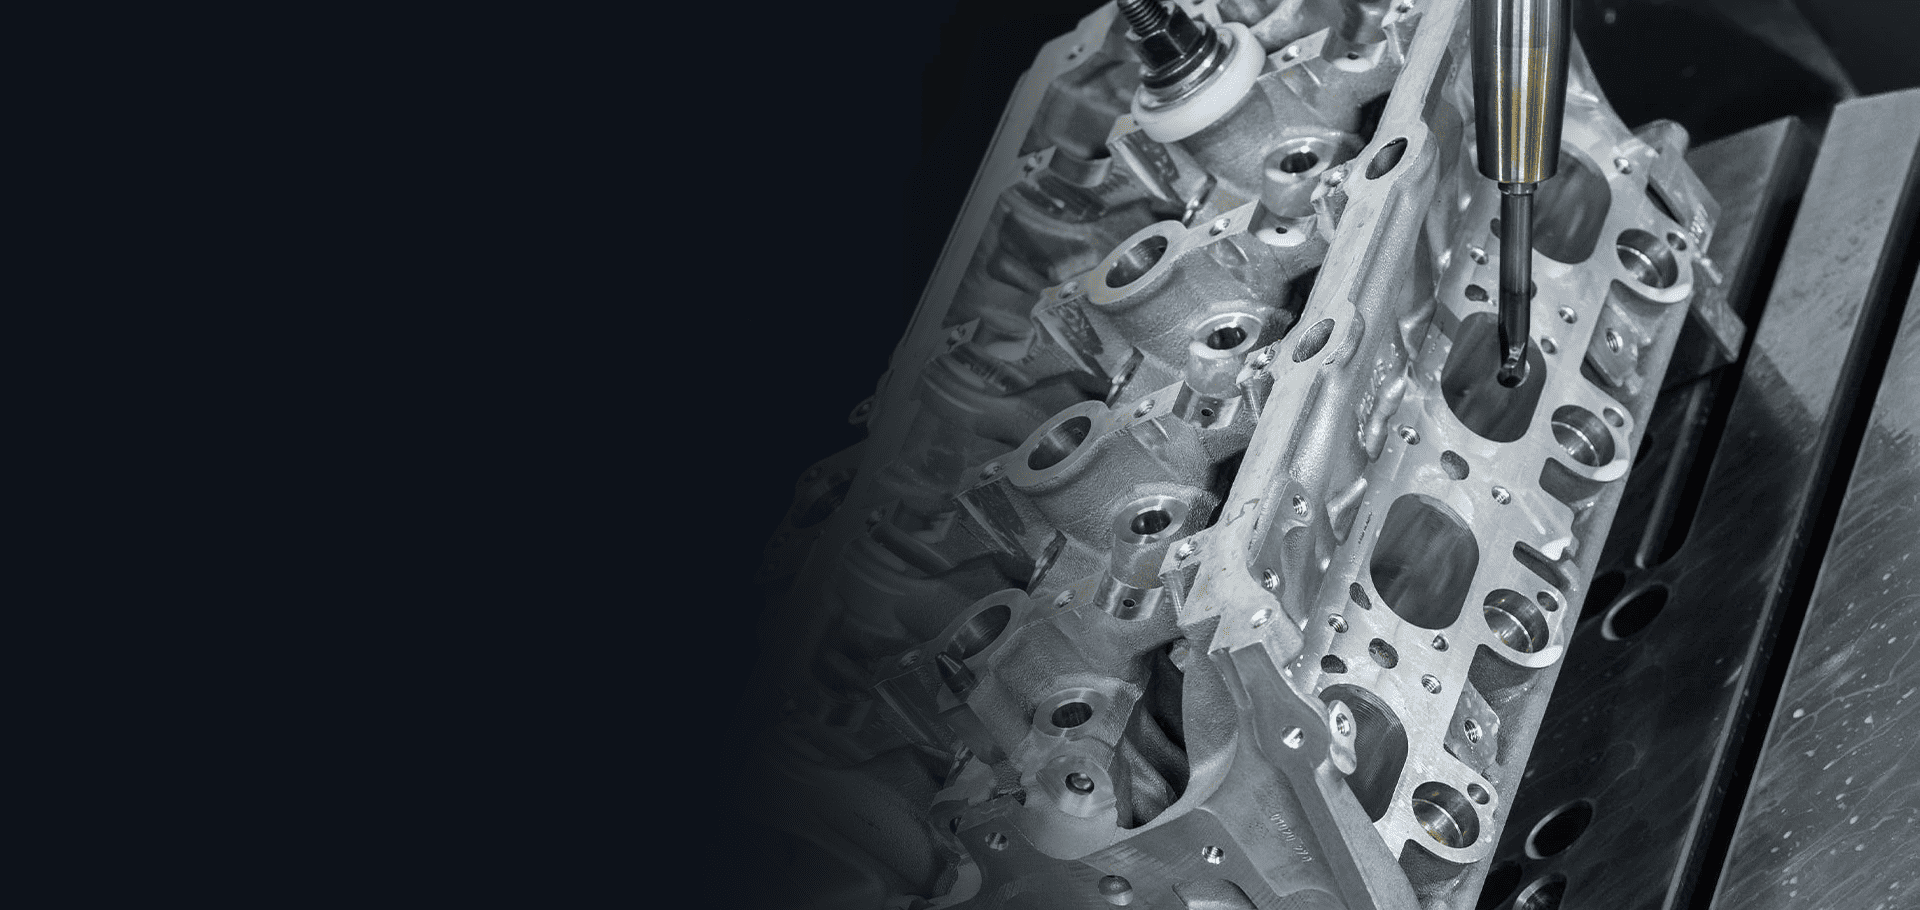
Engine block machining for OEM and Tier programs and motorsport engineering teams. We machine new blocks and block components from castings to your drawing.
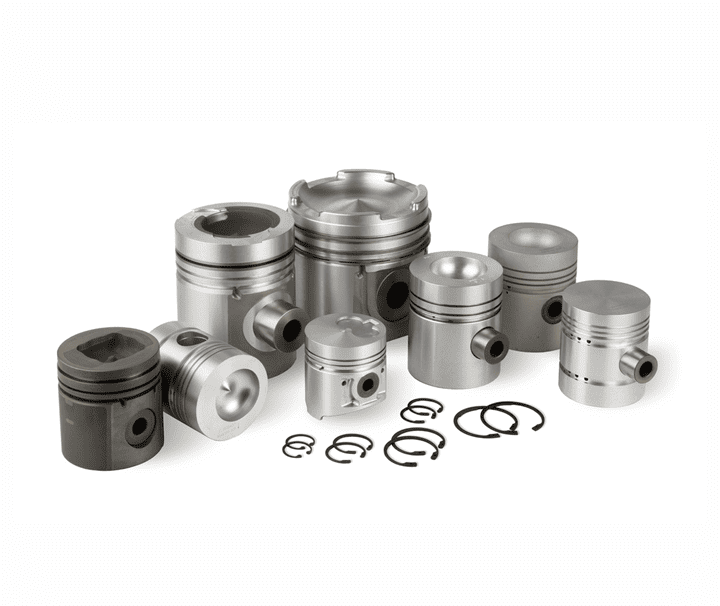
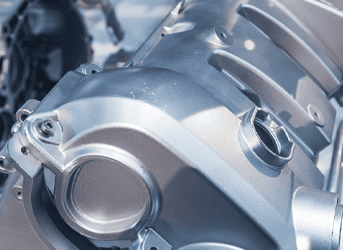
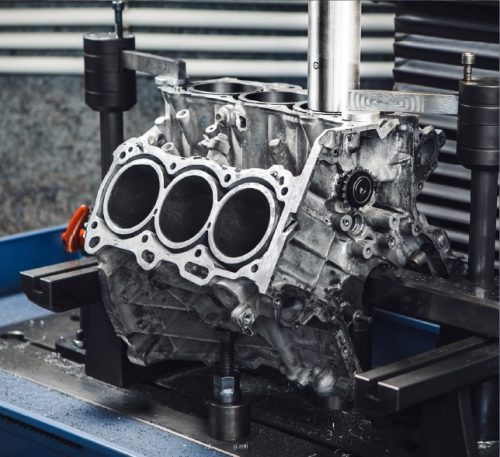
DekAutomotive machines new engine blocks and engine block components from castings to OEM drawings: crankcases, main bearing caps, bedplates and ladder frames, front and timing covers, as part of our powertrain components.
We work for OEM engine departments, Tier 1 and Tier 2 suppliers and motorsport engineering teams, from engineering samples to low-volume and repeat production. When cylinder head machining is in the same program, both parts are fixtured from compatible datums.
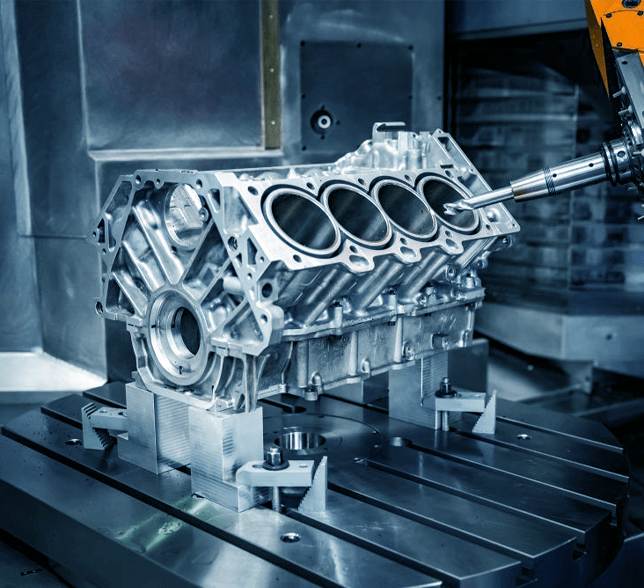
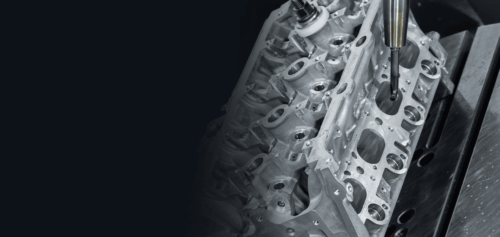
Deck faces, cylinder bores, main bearing line bores, cam tunnel, threaded holes and deep-hole drilling of oil galleries, all machined from datum pads on the casting so each feature stays placed relative to the crank axis.
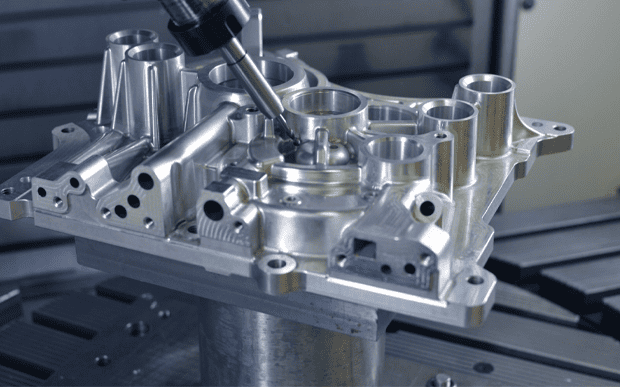
Main bearing caps are machined as a set with the block: caps installed and torqued, then the main bores line bored in one pass along the crank axis so the line bore stays true.
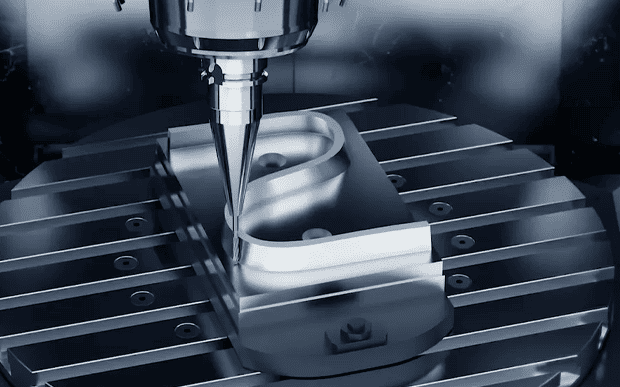
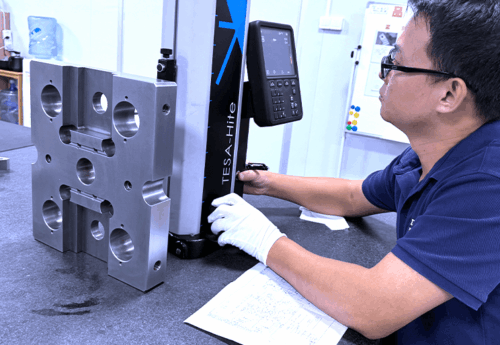
Large flat parts that close the crankcase and carry the main bearing halves. Main bore alignment against the drawing datums is verified by CMM inspection.
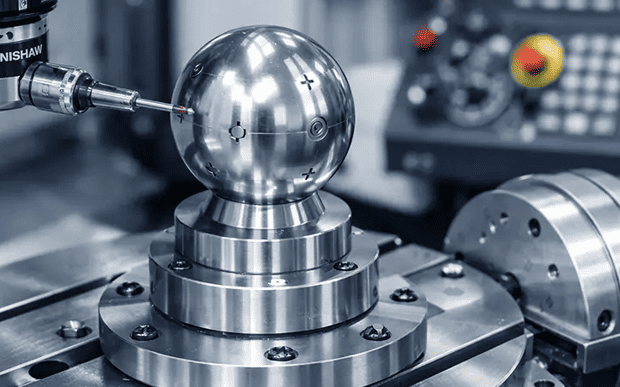
Front and timing covers carry sealing faces, seal bores and bolt patterns that must align with the crank and cam axes of the block they close.
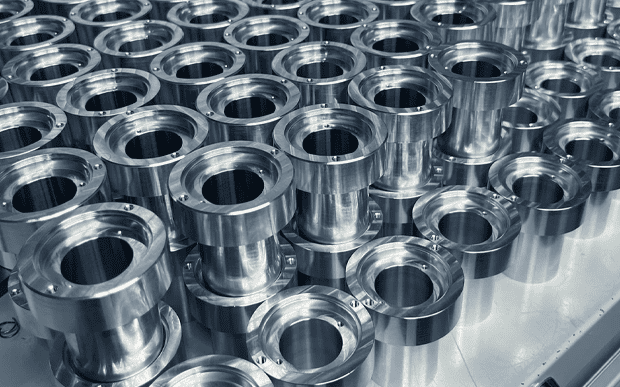
Flat sealing faces and threaded holes on the lower block interface. The pan rail side usually carries the datum pads and dowel holes machined first on the casting.
Cast aluminum blanks for light passenger car and motorsport blocks, with cast-in iron liners, machined to your drawing.
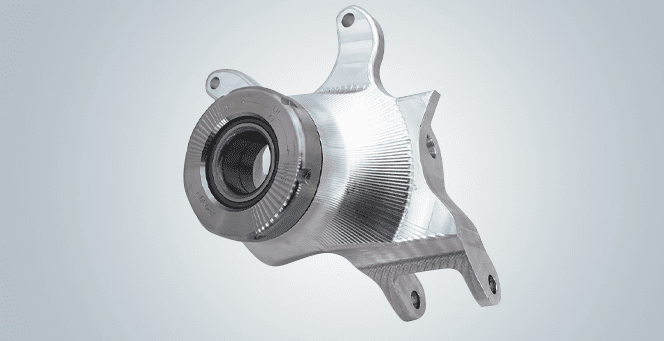
Liners cast into aluminum blocks are bored to size; the aluminum around them needs care against distortion during boring.
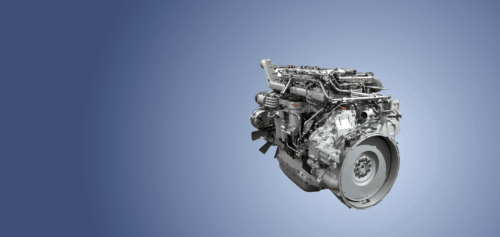
Cast blanks for diesel and commercial vehicle blocks. Gray iron machines well; the as-cast skin carries abrasive scale.
The table summarizes what we machine and check against your drawing and specification. The block design remains your engineering responsibility.
| Manufacturing Parameter | Technical Specification |
|---|---|
| Part types | Blocks, main bearing caps, bedplates, covers |
| Materials | Aluminum A319 / A356, gray cast iron ASTM A48 |
| Blanks | Cast blanks machined to your drawing |
| Critical features | Deck, cylinder bores, main line bores, galleries |
| Tolerancing | Per ASME Y14.5 / ISO 1101 on your drawing |
| Inspection | CMM, bore gauges, thread gauges |
| Documentation | FAI report and MTRs per casting lot, on request |
| Quantities | Engineering samples to repeat production |
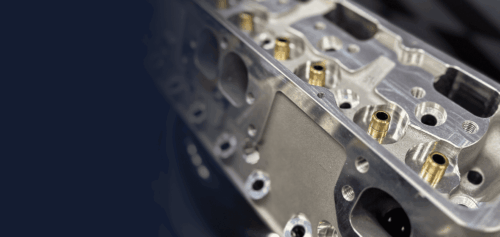
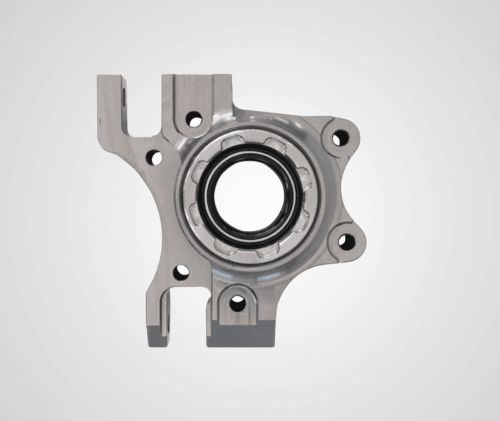
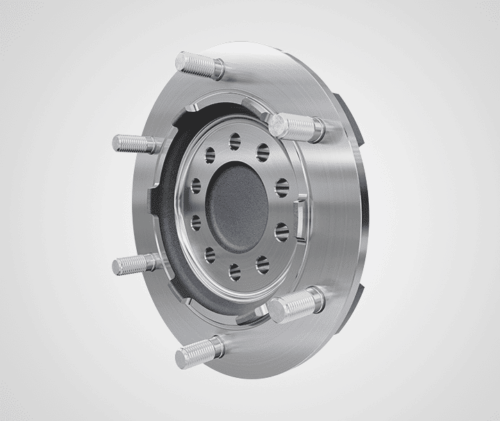
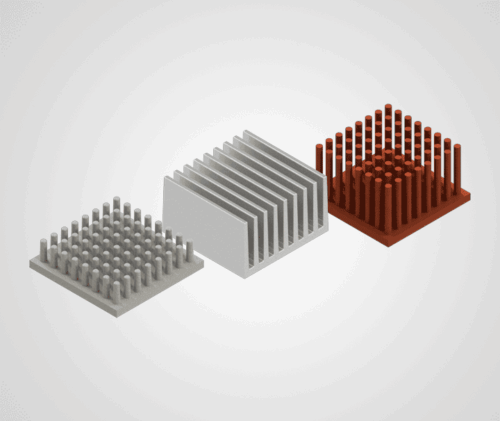
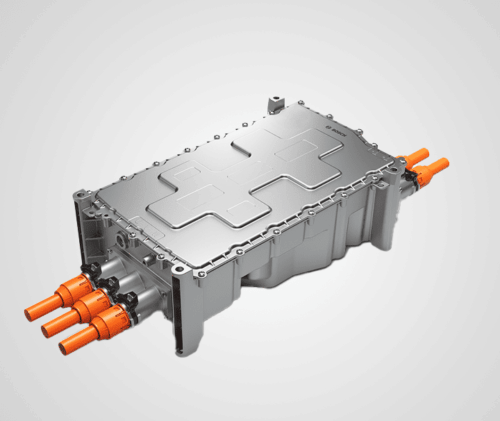

Every bore, deck and gallery is placed from the crank axis datums.

Deck, bores and main bore alignment checked on CMM against your datums.

Engineering samples, validation parts, low-volume and repeat production.
We integrate advanced machining, specialized materials, and surface finishing to deliver mission-critical parts that meet every rigorous automotive standard.
Fill out the form below and our team will get back to you promptly with a personalized quote tailored to your needs.