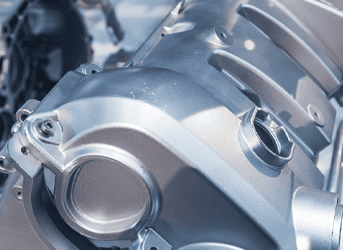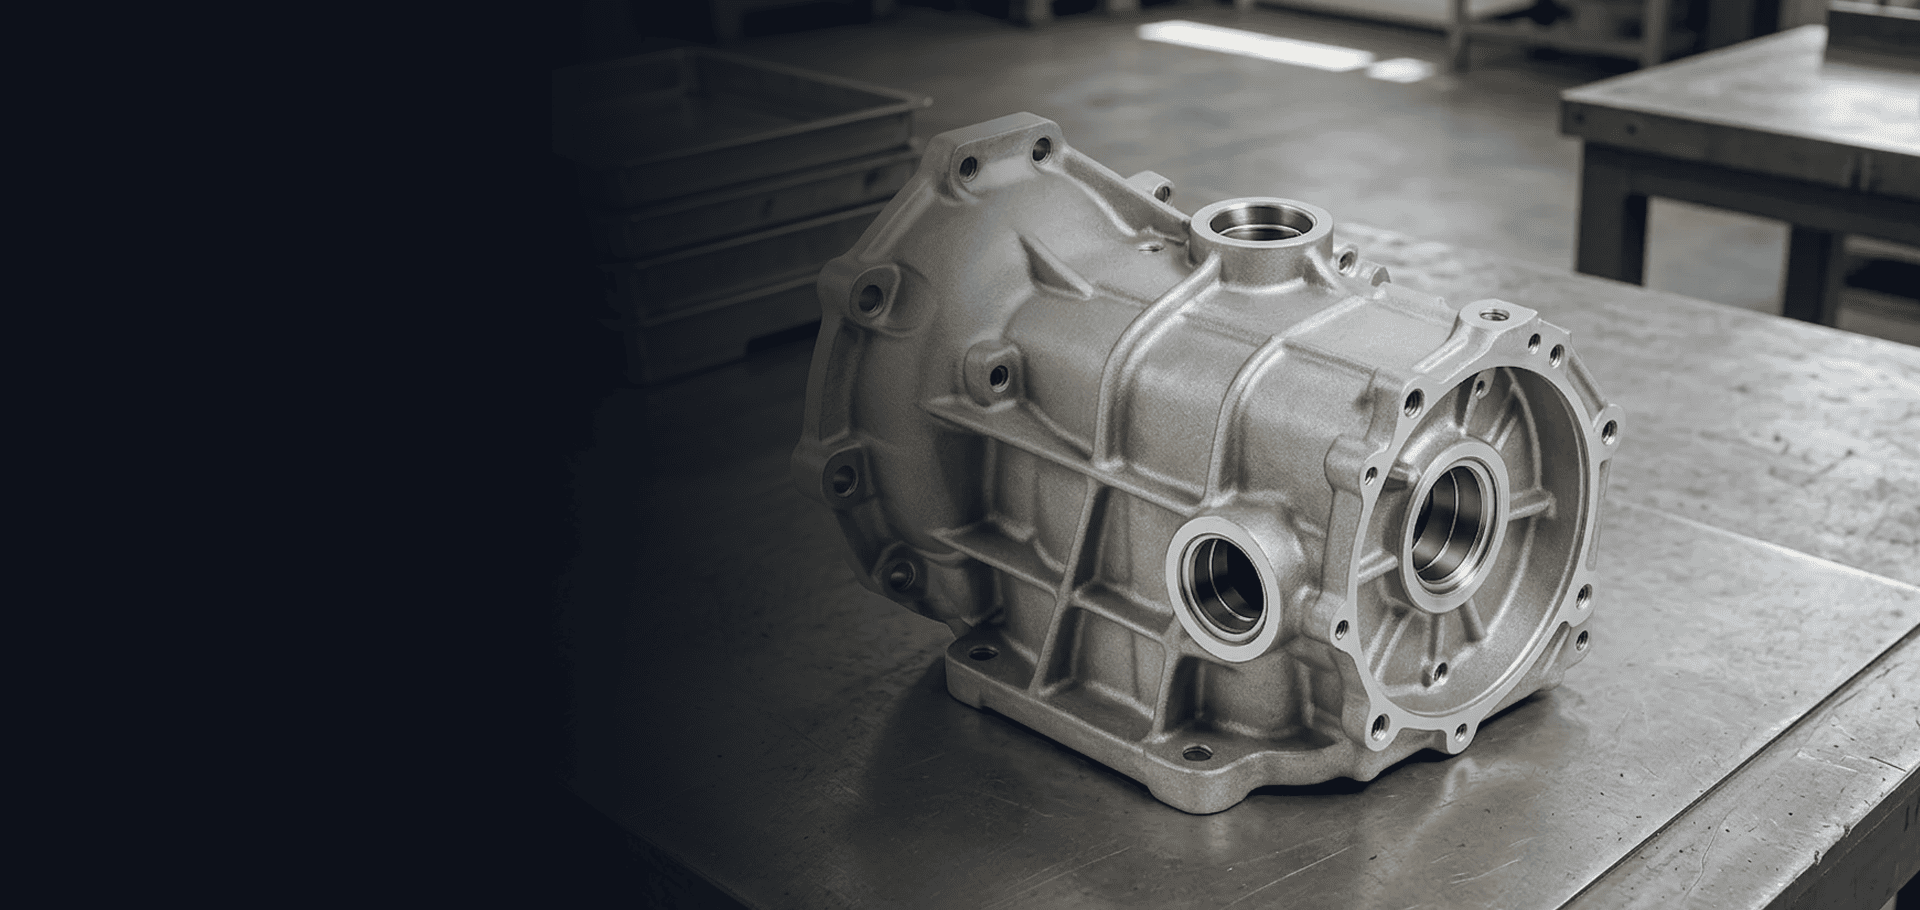
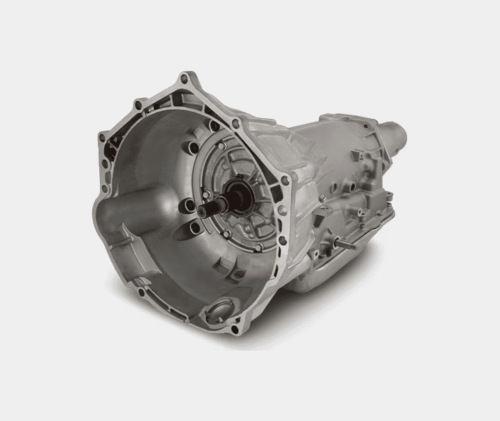
Gearbox housing machining to your drawing for OEM and Tier programs: manual gearbox, DCT and transfer case housings. We machine cast or billet blanks.
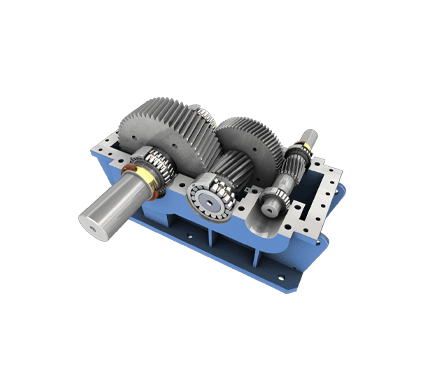
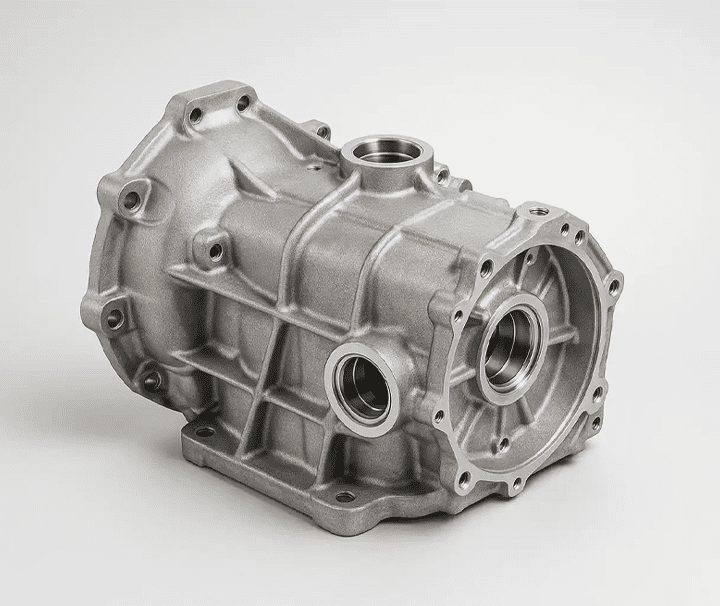
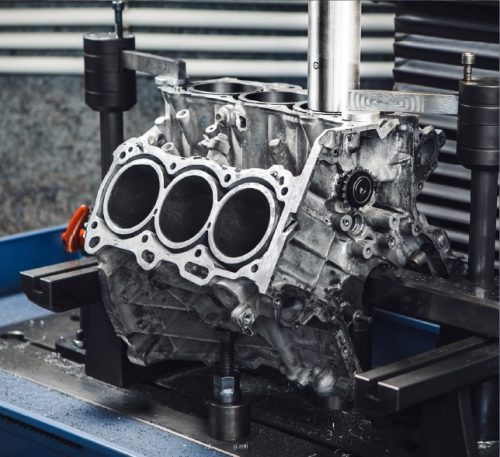
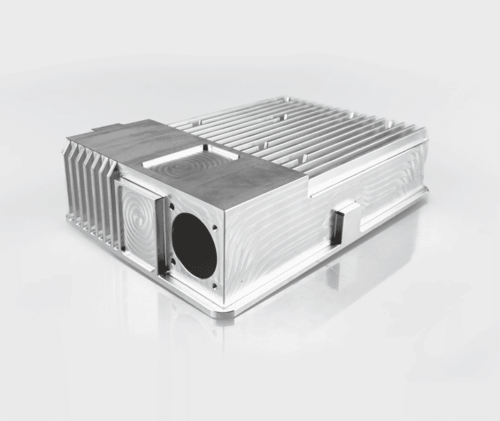
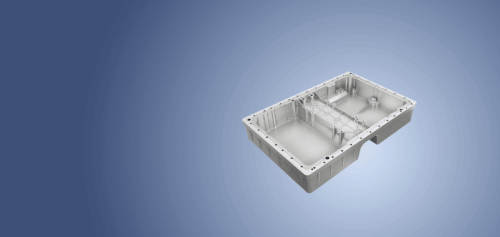
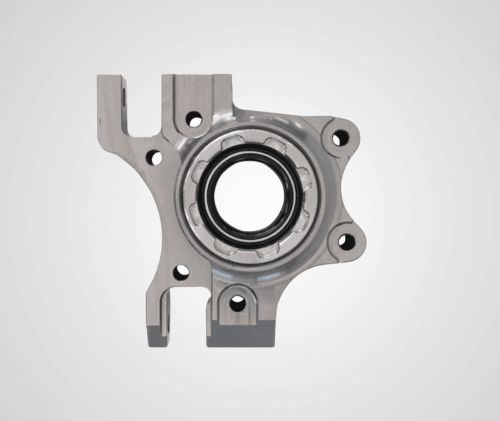
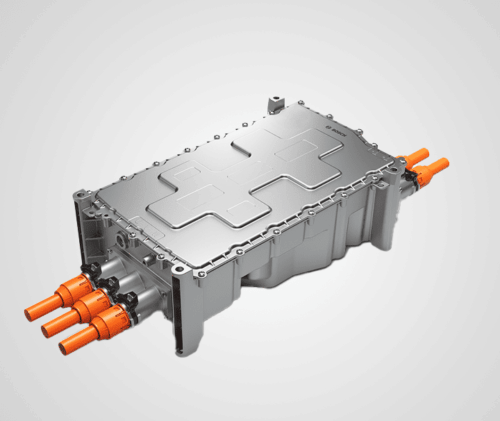
A gearbox housing supports the bearings and shafts, keeps the gears in mesh at the right center distance and contains the oil. We machine it to OEM drawings on cast or billet blanks, within our transmission and gearbox components range.
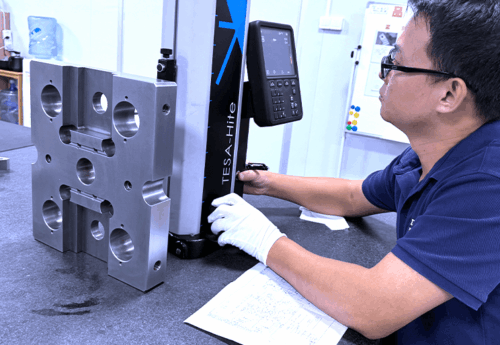
Each program, from engineering samples to repeat production, gets material traceability and CMM verification of bearing bores and faces, following our approach to CMM inspection of complex housings. Inspection reports are available on request.
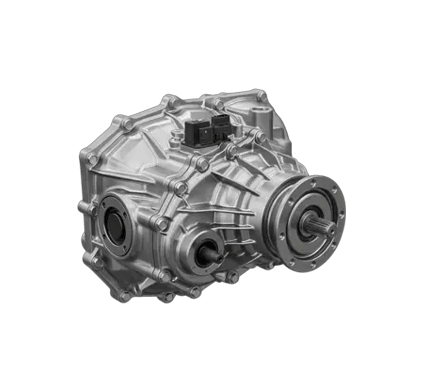
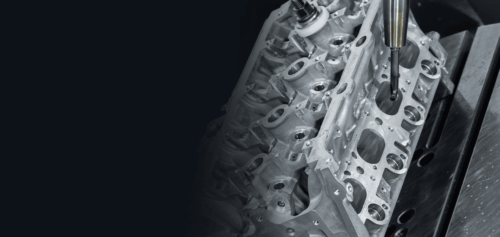
We finish bearing bores and faces in as few setups as possible, on 5-axis or horizontal machining centers, so re-clamping does not lose their relationship. Bores that span both halves are line bored; back boring or back facing reaches features behind a wall.
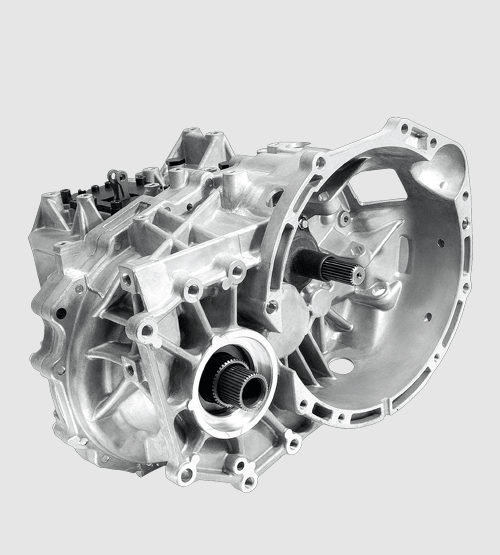
The fixture supports thin walls so that clamping does not move the bores once the part is released. Intersections are deburred and the housing is washed before inspection.
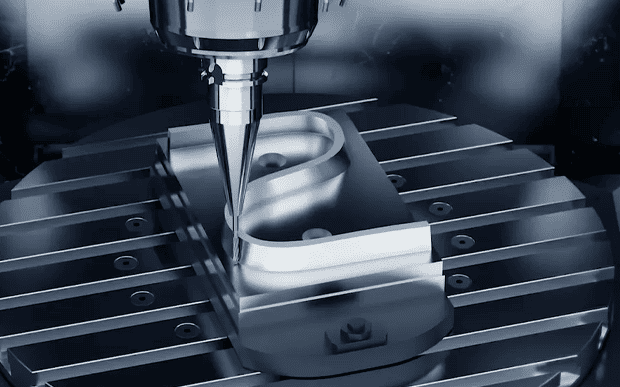
Transmission housings carry bearing bores, split faces and threaded holes like a gearbox housing. We machine them to your drawing with CMM verification; inspection reports are available on request.
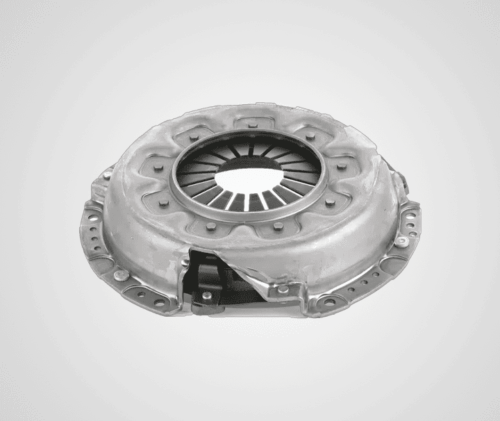
Clutch housings belong to the same transmission and gearbox components range. We machine them to your drawing with material traceability; inspection reports are available on request.
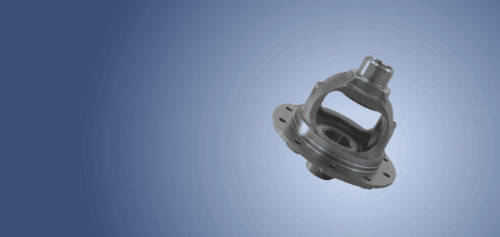
Differential housings and components are grouped with gearbox housings in our transmission range, machined to drawing and CMM verified, with inspection reports on request.
HPDC aluminum blanks for production housings of reducers and transmissions. We do not produce castings; we machine cast blanks to your drawing.
Gravity-cast aluminum blanks for gearbox housings that need higher strength or ductility, machined to your drawing.
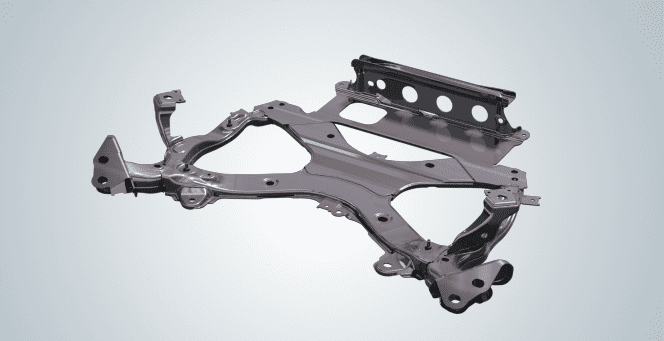
Magnesium cast blanks, machined only where your drawing specifies this alloy for the gearbox housing.
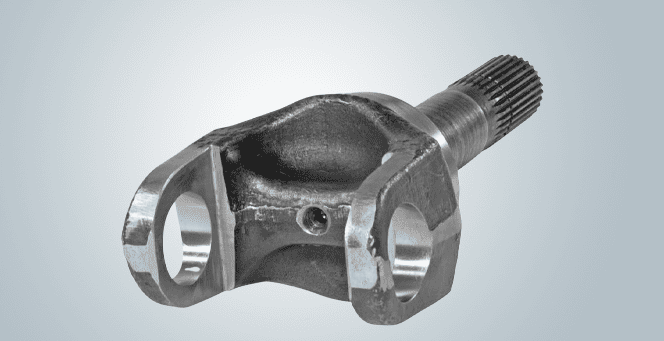
Billet blanks for engineering samples before the casting tool exists, with bearing bores and faces machined to your drawing.
This table summarizes how we machine and inspect gearbox housings; every feature requirement comes from your drawing and your specification.
| Manufacturing Parameter | Technical Specification |
|---|---|
| Part types | Gearbox, DCT and transfer case housings |
| Materials | A380, ADC12, A356-T6, AZ91D; 6061-T6, 7075-T6 |
| Blanks | Cast blanks to your drawing; billet for samples |
| Machines | 5-axis and horizontal machining centers |
| Critical features | Bearing bores, split faces, seal bores, dowel holes |
| GD&T | Per your drawing to ASME Y14.5 or ISO 1101 |
| Inspection | CMM: bore position, coaxiality, face flatness |
| Documentation | FAI, inspection reports and MTRs on request |
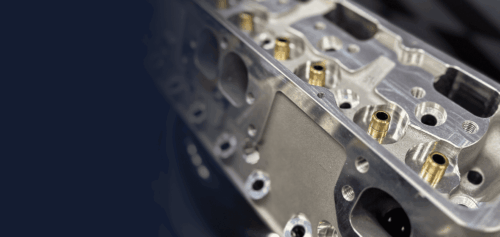
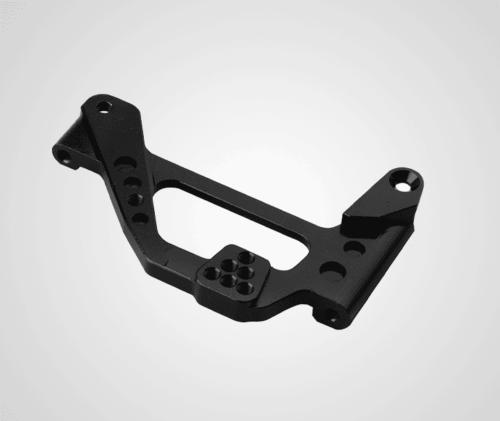
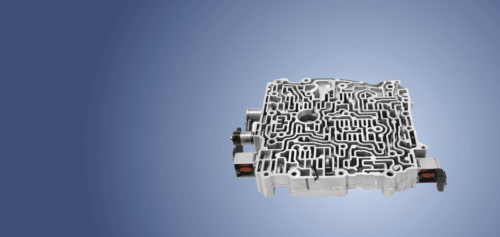
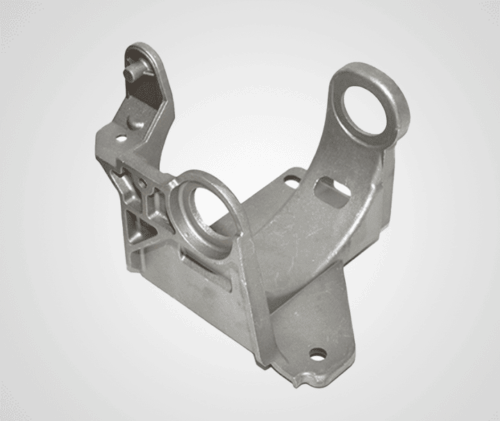

Bore position, coaxiality and face flatness checked by CMM.

Traceable material on every program, MTRs on request.

From billet engineering samples to repeat production.
We integrate advanced machining, specialized materials, and surface finishing to deliver mission-critical parts that meet every rigorous automotive standard.
Fill out the form below and our team will get back to you promptly with a personalized quote tailored to your needs.